Complete Guide to Pipe Counter Boring & Facing Machines: Tube End Preparation, Chamfering & Sizing (2026)
Published: 2026-08-30 | By Gagan Engineering Technical Team
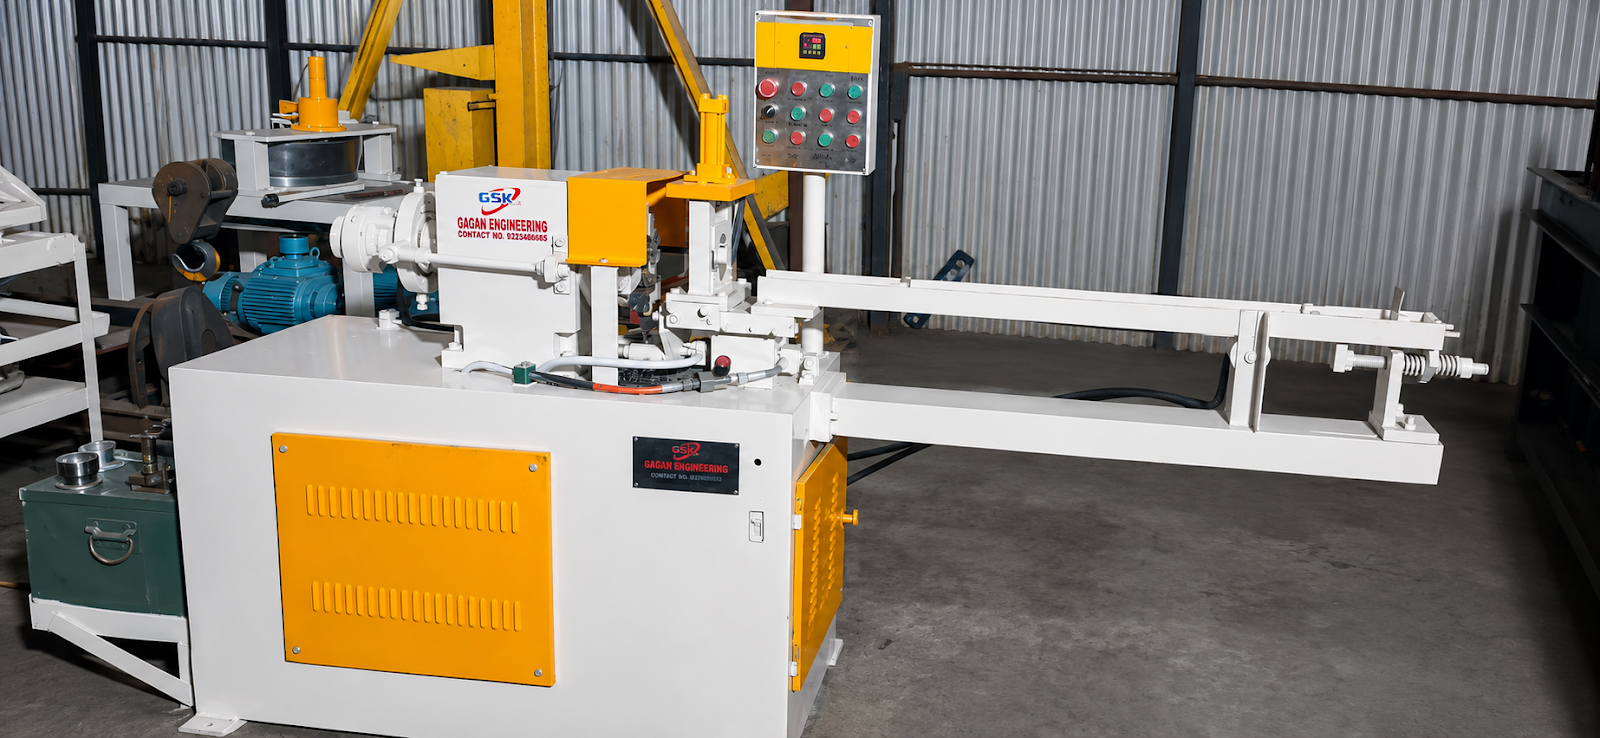
Comprehensive technical guide on industrial pipe end preparation: simultaneous facing, ID counter-boring, and OD weld-prep beveling up to 60 mm OD, VFD spindle drives, and hydraulic clamping systems.
Introduction to Industrial Pipe End Preparation
In modern automotive, boiler, scaffolding, and high-pressure fluid piping manufacturing, rough saw-cut or sheared pipe ends are unacceptable. Burrs, out-of-square cut faces, and inconsistent internal diameters prevent automated robotic welding, lead to leaky flared fittings, and cause premature joint failure.
Achieving perfectly square pipe ends with uniform external weld-prep bevels and calibrated internal counter-bores at mass-production cycle times requires a dedicated Semi-Automatic Pipe Counter Boring and Facing Machine.
At Gagan Engineering Works in Khopoli, Maharashtra, we have engineered high-precision pipe end finishing machinery serving tube manufacturers, automotive exhaust tier-1 suppliers, and structural engineering contractors across India and international markets.
3-in-1 Simultaneous Facing, Chamfering & Boring
The primary advantage of the Gagan Engineering Pipe Counter Boring and Facing Machine is its simultaneous multi-tool single-stroke operation:
- End Perpendicular Facing: Faces the raw pipe end perfectly square (90° ± 0.05 mm) to the tube centerline, removing saw teeth marks and slag.
- External Weld Chamfering: Applies a precision weld-prep chamfer (30°, 37.5°, or 45°) to ensure deep weld penetration in automated robotic or TIG/MIG welding lines.
- Internal ID Counter-Boring: Bores out internal flash, seam weld beads, and sizing variations to an exact depth and diameter, enabling clean press-fit sleeve or plug insertion.
- One Single Rapid Stroke: All three cutting operations occur simultaneously within a rapid 8 to 15-second hydraulic feed cycle.
Technical Comparison: Pipe Counter Boring & Facing Line
| Parameter | Standard Industry Spec | Gagan Engineering Machine |
|---|---|---|
| Maximum Pipe Capacity | Up to 50 mm OD | Up to 60 mm Outside Diameter (OD) |
| Minimum Pipe Capacity | 25 mm OD | 15 mm Outside Diameter (OD) |
| Wall Thickness Range | 1.0 mm to 3.5 mm | 0.8 mm to 6.0 mm (Heavy Gauge Capable) |
| Spindle Motor | 3.0 HP Single Speed | 5.0 HP (3.7 kW) with VFD Speed Control |
| Spindle Speed Range | Fixed 700 RPM | 100 to 1450 RPM Infinitely Variable |
| Clamping System | Manual Screw Clamp | Rigid Self-Centering Hydraulic V-Jaws |
| Hydraulic Power Pack | Shared or None | Dedicated 1.0 HP Unit (60L Reservoir) |
| Cycle Time | 25–40 seconds | 8 to 15 seconds per pipe end |
| Machining Tolerance | ± 0.20 mm | ± 0.05 mm Repeatable Precision |
| Tooling Type | Brazed HSS Tooling | Standard ISO Indexable Carbide Inserts |
Rigid Hydraulic Self-Centering Clamping
Vibration during heavy interrupted cuts degrades surface finish and destroys carbide tool tips. Our machine features a heavy-duty hydraulic self-centering V-clamp driven by a double-acting cylinder. The clamping pressure is fully adjustable via an external hydraulic pressure regulator, allowing the operator to firmly secure heavy-wall boiler tubes without crushing or ovalizing thin 0.8 mm automotive exhaust tubing.
5.0 HP Spindle Drive & VFD Speed Optimization
Different tube materials require distinct surface cutting speeds:
• Mild Steel (MS / ERW): 600 – 900 RPM
• Stainless Steel (SS 304 / 316): 300 – 500 RPM (High torque to prevent work hardening)
• Aluminium & Brass: 1000 – 1450 RPM (Mirror surface finish)
The integrated Variable Frequency Drive (VFD) enables smooth digital potentiometer dial-in of spindle RPM to match the exact pipe diameter and alloy, extending tool insert lifespan by up to 300%.
Standard Indexable Carbide Tooling
The cutter head accommodates standard off-the-shelf ISO indexable carbide inserts. When a cutting edge wears down, the operator simply loosens a Torx screw and rotates the insert to a fresh cutting edge in under 60 seconds without altering the machining depth stop settings or removing the cutter assembly.
Key Industry Applications & Cycle Times
With an operational throughput of 1,500 to 2,400 pipe ends per 8-hour shift, this machine delivers rapid payback across:
1. Automotive Components: Shock absorber cylinders, exhaust downpipes, steering column tubes, propeller shafts.
2. Boiler & Heat Exchanger Fabrication: Tube-to-tubesheet weld prep and internal expander entry sizing.
3. Scaffolding & Structural Tubing: Cuplock scaffolding pipe spigots and structural steel column ends.
4. Hydraulic Cylinders: Honed tube end prep for cylinder cap welding.
For detailed pricing, custom tooling layouts, and trial sample demonstrations, view our Semi-Automatic Pipe Counter Boring and Facing Machine Product Page or call our technical works at +91 83294 65245.